Aspire International is an export-oriented food manufacturer based in Punjab, India, specialising in honey, fruit jams, value-added honey products, private-label food manufacturing and innovative single-serve formats. We support importers, distributors, retailers, foodservice companies and private brands with products developed around the requirements of international supply chains.
Aspire International is a honey exporter and fruit jam exporter from India with manufacturing capabilities focused on private-label, OEM and B2B food supply. Export projects may include product specification, formulation, packaging selection, label coordination, manufacturing, traceability, secondary packaging and export documentation according to the agreed buyer and destination-market requirements.
More Than Shipping Products Overseas
A dependable food exporter needs to understand the entire journey between manufacturing and the destination market. Aspire International approaches export supply as a coordinated system involving product specifications, food safety, packaging engineering, traceability, case configuration, private-label execution and commercial documentation.
Product Manufacturing
Controlled manufacturing of honey, fruit jams, value-added honey products and selected portion-controlled food formats.
Private Label
Products can be developed for importers, distributors, retailers and food brands under buyer-owned or custom branding.
Export Packaging
Primary packaging, secondary corrugated cases and selected retail-ready configurations can be engineered around the product.
Market Adaptation
Product specifications, pack configuration and labelling requirements can be evaluated according to customer and destination-market requirements.
Designed Around the International Buyer
Aspire International’s export manufacturing model is particularly suited to professional buyers who require repeatable specifications, defined packaging, commercial documentation and reliable product presentation rather than a generic domestic-market product.
Honey Exporter & Fruit Jam Exporter from India
Aspire International concentrates its export manufacturing capabilities in categories where sourcing, processing, packaging and private-label development can be closely integrated.
Honey Exporter for Retail, Private Label & B2B Supply
Aspire International works as an export-oriented honey manufacturer and honey exporter from India, connecting responsible honey sourcing with controlled processing, packaging and B2B supply.
Honey is sourced through relationships extending across important honey and agricultural regions including Punjab, Haryana, Himachal Pradesh, Rajasthan, Uttarakhand and other sourcing areas. The company promotes scientific beekeeping, responsible harvesting, hygienic handling and traceability throughout its supply network.
- Retail honey packaging
- Private label honey
- OEM honey manufacturing
- Foodservice honey formats
- Bulk and institutional supply
- Single-serve honey formats
- Value-added honey products
- Custom packaging development
Fruit Jam Exporter for Retail, Foodservice & Private Label
Aspire International is developing its international supply platform as a fruit jam manufacturer and jam exporter from India for buyers seeking retail jars, portion-control formats, private-label packs and other commercially packaged fruit products.
Fruit quality, processing behaviour, packaging and finished-product consistency are considered together. Aspire International’s sourcing philosophy encourages responsible agriculture, suitable harvest maturity, hygienic handling and stronger links between farmers and food processing.
- Mixed fruit jam
- Strawberry jam
- Apricot jam
- Pineapple jam
- Mango and fruit variants
- Retail jam jars
- Single-serve jam portions
- Private label fruit jam
Your Brand. Our Manufacturing & Export Infrastructure.
A major focus of Aspire International is private-label and contract food manufacturing. The objective is to give international buyers a practical route from product requirement to commercially packed, export-ready finished goods.
Product Definition
Define product type, target pack, specification, positioning, intended market and commercial requirements.
Packaging Development
Match primary packaging, pack size, closure, label format, secondary carton and case quantity to the project.
Brand Execution
Coordinate buyer-supplied or jointly developed artwork with the physical packaging configuration.
Manufacturing
Manufacture under defined product specifications, process controls, traceability requirements and quality checks.
Export Packing
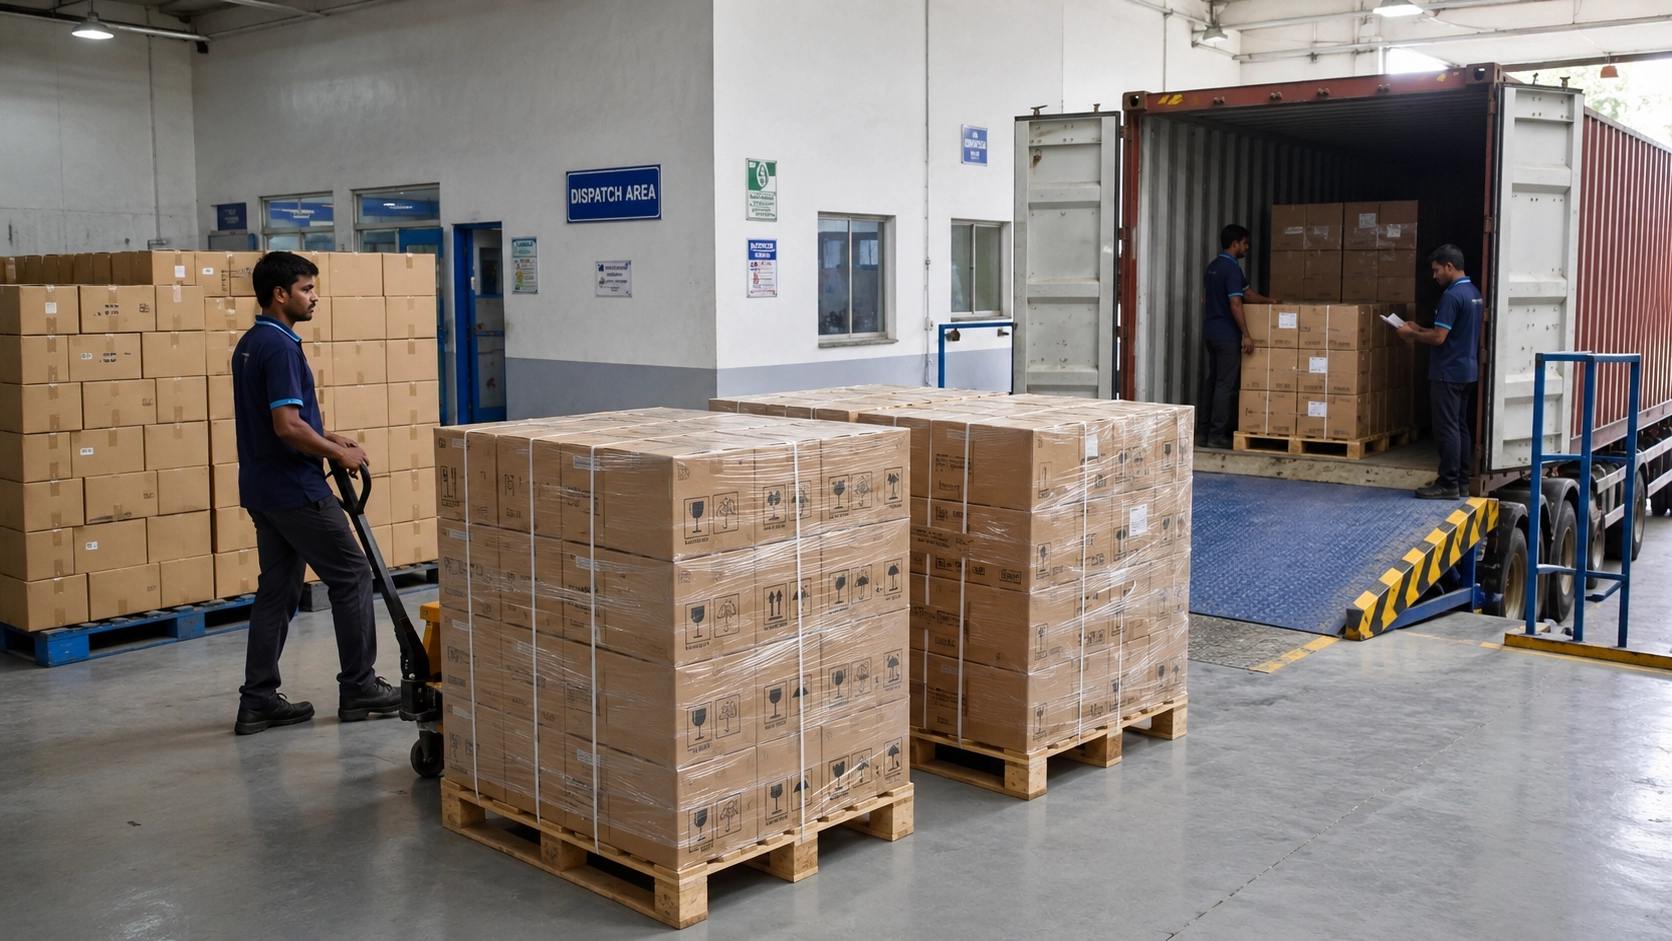
Configure cases and secondary packaging for distribution, palletisation, handling and international transportation.
Commercial Supply
Coordinate agreed documentation, order preparation and shipment requirements with the international buyer.
How an Export Project Moves Through Aspire International
International food procurement often involves more variables than simply selecting a product. The product, label, packaging, case configuration, analytical requirements and commercial documents should be aligned before regular supply begins.
Buyer Requirement
Market, product, pack size, quantity and commercial requirement are reviewed.
Technical Review
Specification, formulation, packaging and applicable buyer requirements are evaluated.
Pack Development
Primary package, label format, case quantity and secondary packaging are established.
Approval
Commercially relevant product and packaging details are finalised before production.
Manufacturing
Production is carried out against defined parameters with traceability and quality controls.
Export Preparation
Finished goods, cases and agreed documentation are prepared for the shipment.
Packaging Designed Beyond the Factory Gate
A food package may look excellent on the filling line and still fail during warehousing, pallet movement, container transportation or retail distribution. Aspire International treats export packaging as part of the engineered product system.
The company’s in-house secondary packaging capabilities allow corrugated shipper cartons to be considered around pack dimensions, product weight, case count, distribution conditions and merchandising requirements.
This is especially relevant for glass jars, PET containers, squeeze packs, portion packs and multipacks that may travel thousands of kilometres before reaching the final retail environment.
Explore Packaging CapabilitiesPrimary Packaging
Jar, bottle, squeeze pack, portion pack or other suitable product-contact packaging based on the commercial project.
Secondary Packaging
Corrugated export cases engineered around dimensions, weight, protection and handling requirements.
Retail Ready Packaging
Selected products can be evaluated for shelf-ready or retail-ready case structures.
Buyer Identification
Cases may incorporate agreed product codes, barcodes, shipping marks, handling information and customer branding.
A Honey and Jam Exporter Must Deliver More Than Product
International buyers depend on systematic manufacturing controls, traceability and documented food-safety practices. Aspire International operates with an FSSC 22000-certified food manufacturing system for honey and fruit jams and develops products within the regulatory and buyer frameworks relevant to the intended supply programme.
FSSC 22000 Food Safety System
Systematic controls support food safety management, process discipline, traceability, documented procedures and continual improvement.
Defined Product Specifications
Export supply can be developed against defined physical, chemical, packaging and commercial specifications agreed for the project.
Traceability
Raw-material sourcing, production information and finished-product identification form important parts of the manufacturing system.
Quality Checkpoints
Defined parameters and measurable production controls support repeatability across manufacturing batches.
Destination Requirements
Product formulation, analytical requirements, packaging and labelling may require adaptation depending on the buyer and destination market.
Buyer Documentation
Specifications and supporting documents can be coordinated according to the commercially agreed requirements of the export programme.
Product, Packaging & Documentation Must Work Together
The exact documentation for an international shipment varies by product, destination, customer, logistics route and applicable regulatory requirements. Aspire International therefore evaluates documentation as part of each commercial export project rather than assuming one document set fits every country.
| Export Area | What May Need to Be Defined | Aspire International Approach |
|---|---|---|
| Product Specification | Product description, ingredients, physical and quality parameters, pack format and shelf-life requirements. | Commercial and technical requirements are reviewed before regular production. |
| Label Information | Product identity, ingredients, nutrition information, declarations, country-specific information and buyer branding. | Label requirements are coordinated according to the agreed destination and buyer brief. |
| Case Configuration | Units per case, dimensions, weight, barcodes, shipping marks and handling symbols. | Secondary packaging can be engineered together with the finished product. |
| Commercial Documents | Documents required for the applicable transaction and shipment. | Prepared according to the agreed trade arrangement and applicable export requirements. |
| Buyer Documentation | Product specifications, manufacturing information or supporting documents required by the commercial programme. | Requirements are reviewed during buyer onboarding. |
Documentation requirements differ by destination and shipment. Final requirements should be confirmed for each specific order and importing market.
Export Products Should Be Developed for Their Destination
A retail honey jar, foodservice pack or fruit jam sold in one market may require a different net quantity, language, nutrition format, barcode, carton configuration, formulation specification or merchandising format in another.
Aspire International therefore approaches international projects as market-specific manufacturing programmes rather than assuming a single domestic configuration should be exported everywhere.
Reduce Fragmentation Across the Export Supply Chain
Export projects become unnecessarily complicated when the food manufacturer, packaging supplier, carton converter, designer and exporter operate as disconnected parties. Aspire International’s operating model is intended to coordinate more of these elements around the finished product.
Food Manufacturing
Honey, fruit jam and selected value-added or portion-controlled food manufacturing.
Packaging Engineering
Packaging can be developed around product behaviour, case count, transportation and merchandising requirements.
Export Preparation
The manufactured product, case configuration and agreed documentation can be coordinated within the same commercial programme.
Export Quality Begins Before Manufacturing
For Aspire International, food quality begins with the agricultural supply chain. Honey quality is influenced by bee health, surrounding flora, harvesting practices, apiary hygiene and post-harvest handling.
Fruit quality is similarly influenced by variety, harvest maturity, orchard management, handling, transport and the characteristics of the raw material entering processing.
Scientific Beekeeping
Aspire International encourages responsible apiary management, hygienic handling and careful harvesting.
Traceable Sourcing
Relationships with beekeepers, farmers and supply partners support better visibility upstream.
Responsible Agriculture
Agricultural partners are encouraged to use technically sound cultivation and post-harvest practices.
Long-Term Relationships
Stable supplier relationships support communication, consistency and continuous quality improvement.
Information That Helps Us Evaluate Your Requirement Faster
A clear buyer brief allows the manufacturing and export team to evaluate technical feasibility, packaging requirements and commercial suitability more efficiently.
You do not need to have every specification finalised before contacting Aspire International. Early-stage private-label and product-development enquiries can also be discussed.
Continue Your Supplier Evaluation
Manufacturing
Learn how Aspire International approaches food manufacturing and process control.
ManufacturingQuality
Review food-safety systems, controls and the manufacturing quality philosophy.
Quality & Food SafetyPackaging
Explore packaging formats and the engineering approach to primary and secondary packaging.
PackagingPrivate Label
Develop honey, fruit jam and related products under your own brand.
Private LabelFrequently Asked Questions About Aspire International Exports
Is Aspire International a honey exporter from India?
Yes. Aspire International is an export-oriented food manufacturer in Punjab, India, with honey manufacturing and B2B export supply among its core commercial activities. Projects can include retail honey, private-label honey, foodservice formats, bulk formats and selected value-added honey products.
Is Aspire International a fruit jam exporter?
Aspire International manufactures fruit jams for B2B, private-label and export-oriented supply. Packaging can include retail jars, portion formats and buyer-specific configurations depending on the commercial project.
Can Aspire International export honey under my own brand?
Yes. Private-label honey manufacturing is an important part of Aspire International’s B2B model. The project can cover product specification, pack selection, branding coordination, manufacturing, secondary packaging and export preparation.
Can fruit jam be manufactured under a private label?
Yes. Aspire International can evaluate private-label fruit jam projects involving product variant, packaging format, net quantity, artwork, case configuration and other buyer requirements.
What type of international buyers can work with Aspire International?
Suitable buyers can include food importers, distributors, supermarket sourcing teams, wholesalers, cash-and-carry businesses, private-label companies, foodservice suppliers, hospitality suppliers, institutional buyers and international food brands.
Does Aspire International manufacture export packaging?
Aspire International has secondary packaging capabilities that support the development of corrugated shipper cases around product dimensions, weight, case quantity, transportation and merchandising requirements.
Does Aspire International have an FSSC 22000 food-safety system?
Aspire International operates with an FSSC 22000-certified food manufacturing system for honey and fruit jams, supporting systematic food-safety management, traceability, process control and continuous improvement.
Can packaging and labels be adapted for different countries?
Depending on the project, destination and buyer requirement, product specifications, formulations, packaging configurations, labelling information and documentation may require market-specific adaptation. The requirements should be reviewed before commercial production.
Does Aspire International supply only large supermarket chains?
No. The company’s B2B manufacturing model can be relevant to different types of professional buyers, including importers, distributors, wholesalers, private brands, foodservice companies and institutional procurement businesses. Commercial feasibility depends on the specific product and order requirement.
How do I request an export quotation?
Send Aspire International the intended destination, product, pack size, preferred packaging, estimated quantity and whether the requirement is for private label or another B2B programme. This allows the team to evaluate the enquiry more effectively.
Looking for a Honey Exporter or Fruit Jam Exporter from India?
Share your target country, product, packaging format and expected requirement with Aspire International. Whether you are developing a private-label honey brand, sourcing fruit jam, evaluating foodservice portions or building a new international retail programme, the discussion can begin with your commercial requirement.